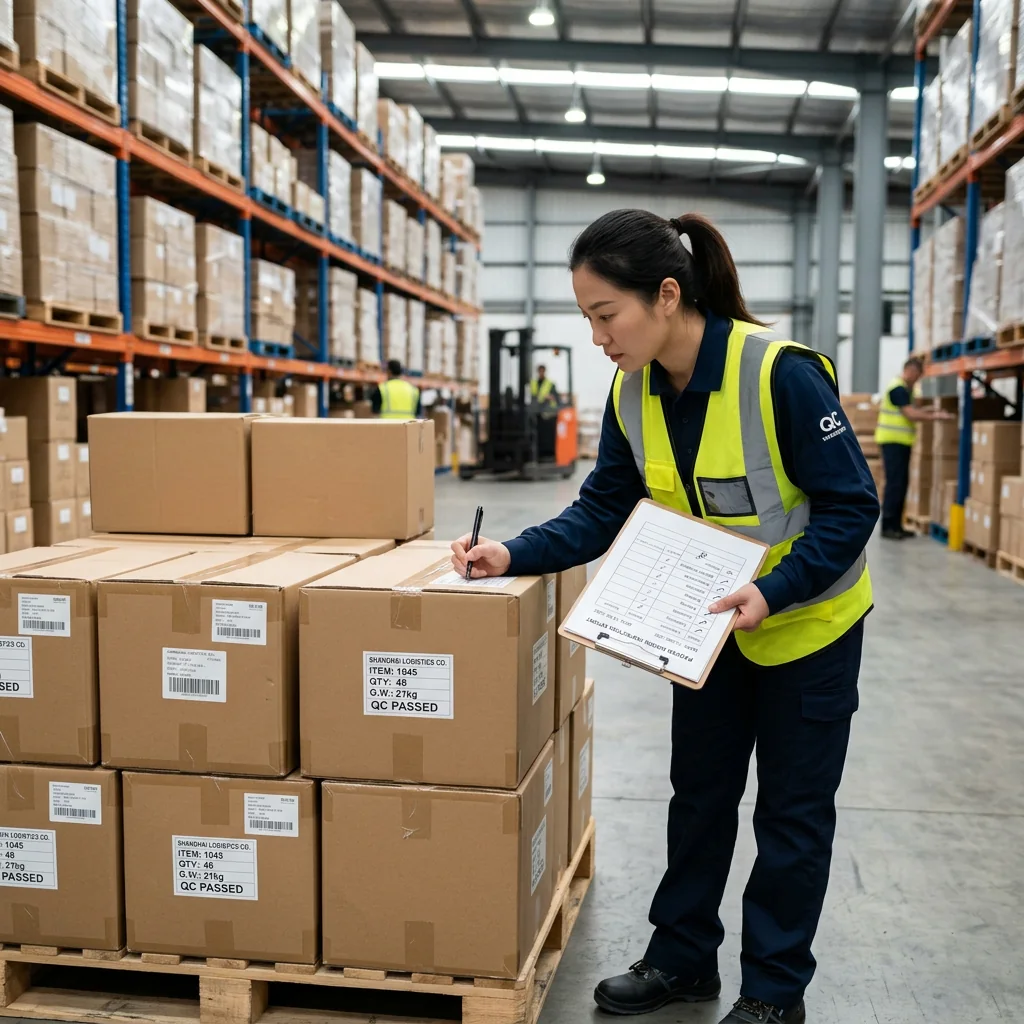
An inspection report that says "quality is good" is worth nothing. The value is in the sampling plan, the measured dimensions and the defect classification — three things that have to be decided before the inspector arrives, not after.
Timing, and why it is usually wrong
Agree the required completion and packing condition with the inspection provider before booking. Make the full declared lot accessible for random selection and leave time to inspect packaging, resolve defects and re-inspect before shipment. Record any units that were not available; a partial inspection must not be presented as covering the entire order.
Confirm inspector availability, factory access, production readiness and the forwarder’s cargo cutoff together. Obtain an actual booking date rather than assuming a fixed lead time, especially around holidays.
Agree inspection, release and payment milestones in the purchase contract. An inspection report does not replace contractual remedies, and payment should follow the agreed evidence and acceptance process.
AQL, in the amount of detail you actually need
An attribute sampling plan can be used to decide whether to accept a lot. If the contract uses ISO 2859-1, state the agreed edition, inspection level, normal/tightened/reduced regime, lot size and acceptance quality limit for each defect class. AQL is a parameter of the plan, not a guarantee of the delivered defect percentage.
Choose the inspection level and defect-specific acceptance criteria with the quality specialist for this product. Define critical, major and minor defects before inspection; safety or regulatory requirements may require additional testing or screening beyond the sampling plan.
Do not read an AQL value of 2.5 as permission to deliver 2.5% defective goods. Obtain the sample-size code, sample size and acceptance/rejection numbers from the tables for the exact agreed plan. An explicit rule to reject on any observed critical defect must be documented separately; finding none in a sample does not prove none exist in the lot.
Choose acceptance criteria according to defect severity, product risk, contractual requirements and the plan’s operating characteristics. Do not apply the same AQL or inspection level to every electrical, clothing or cosmetic product.
Here is what most buyers miss: the defect classification matters more than the AQL number. If a loose thread and a non-functioning switch are both classified as "minor", a 4.0 AQL is meaningless. Write the classification yourself.
What to put in the inspection brief
Send the inspector a document, not an email thread. It should contain:
- Your approved sample photographs, with the dimensions you measured marked on them
- The specification: material, grade, dimensions with tolerances, weight, colour reference
- Defect classification — an explicit list of what counts as critical, major and minor for this product
- Packaging spec: inner packing, carton construction, units per carton, carton dimensions and gross weight
- Label and carton mark artwork, including barcode
- Any function test you want performed, and how many units to test
- Your AQL levels
Review the brief whenever the product, supplier, packaging or destination requirements change.
What the inspector checks on site
Quantity. Cartons counted, a sample of cartons opened and counted. Short shipments are found here or not at all.
Workmanship. The sampled units examined against the defect list, with defects photographed and tallied by class.
Dimensions and weight. Measured with instruments, against your tolerances. This is where material substitution shows up — a part moulded in a cheaper resin often comes out measurably lighter.
Function. Whatever the product is supposed to do, on a defined number of units.
Packaging and drop test. Carton construction, seal quality, and on most consumer goods a drop test from a specified height on specified faces.
Marking. Barcode scanned — actually scanned, not visually compared. Carton marks, country of origin, any market-specific label.
Reading the report
Look at the photographs before the conclusion. Every report has photographs of defects; the conclusion is a judgement applied to a rule you set.
Read the actual sample size, observed defect counts and the specified acceptance/rejection rule alongside the result. A pass is a lot-disposition decision under that plan; it is not a measurement or guarantee of the defect rate of every unit shipped.
Check that the report states the actual quantity found packed. Check that the measured dimensions are recorded as numbers rather than ticked as "conforms". A report full of tick-boxes and no measurements was produced by someone who did not measure.
When it fails
You have four options and should decide which one you want before you tell the factory.
Rework and re-inspect. The usual outcome. Agree in writing who pays for the second inspection — the answer should be the factory, and this should have been in the original terms.
Sort and ship the good units. Works where defects are separable and you can accept a short shipment.
Accept with a discount. Appropriate for cosmetic issues on goods you can still sell. Get the discount agreed before release, not after arrival.
Reject or seek another remedy. The available remedies depend on the agreed contract, applicable rules and nature of the nonconformity. Follow the notice and claim procedure rather than assuming payment alone determines the outcome.
The limits
Inspection is a sample of finished goods at one moment. It will not tell you the resin was recycled rather than virgin, it will not catch a problem that only appears after six months of UV exposure, and it does not verify anything about the batch produced after the inspector leaves.
Material claims may require laboratory testing with an agreed method, specimen preparation and report scope. Request a laboratory quote and confirm whether the tests apply to the production batch; inspection alone cannot verify chemical composition or long-term durability.
Send us your product spec and order quantity and we will draft the defect classification for you — that is the part buyers most often get wrong, and it is the part that determines whether the inspection means anything.
Sampling references and next step
See the ISO 2859-1 standard overview and NIST introduction to acceptance sampling. Use the licensed tables for the edition specified in your contract. Share your product specification and proposed inspection scope for a scope review.